
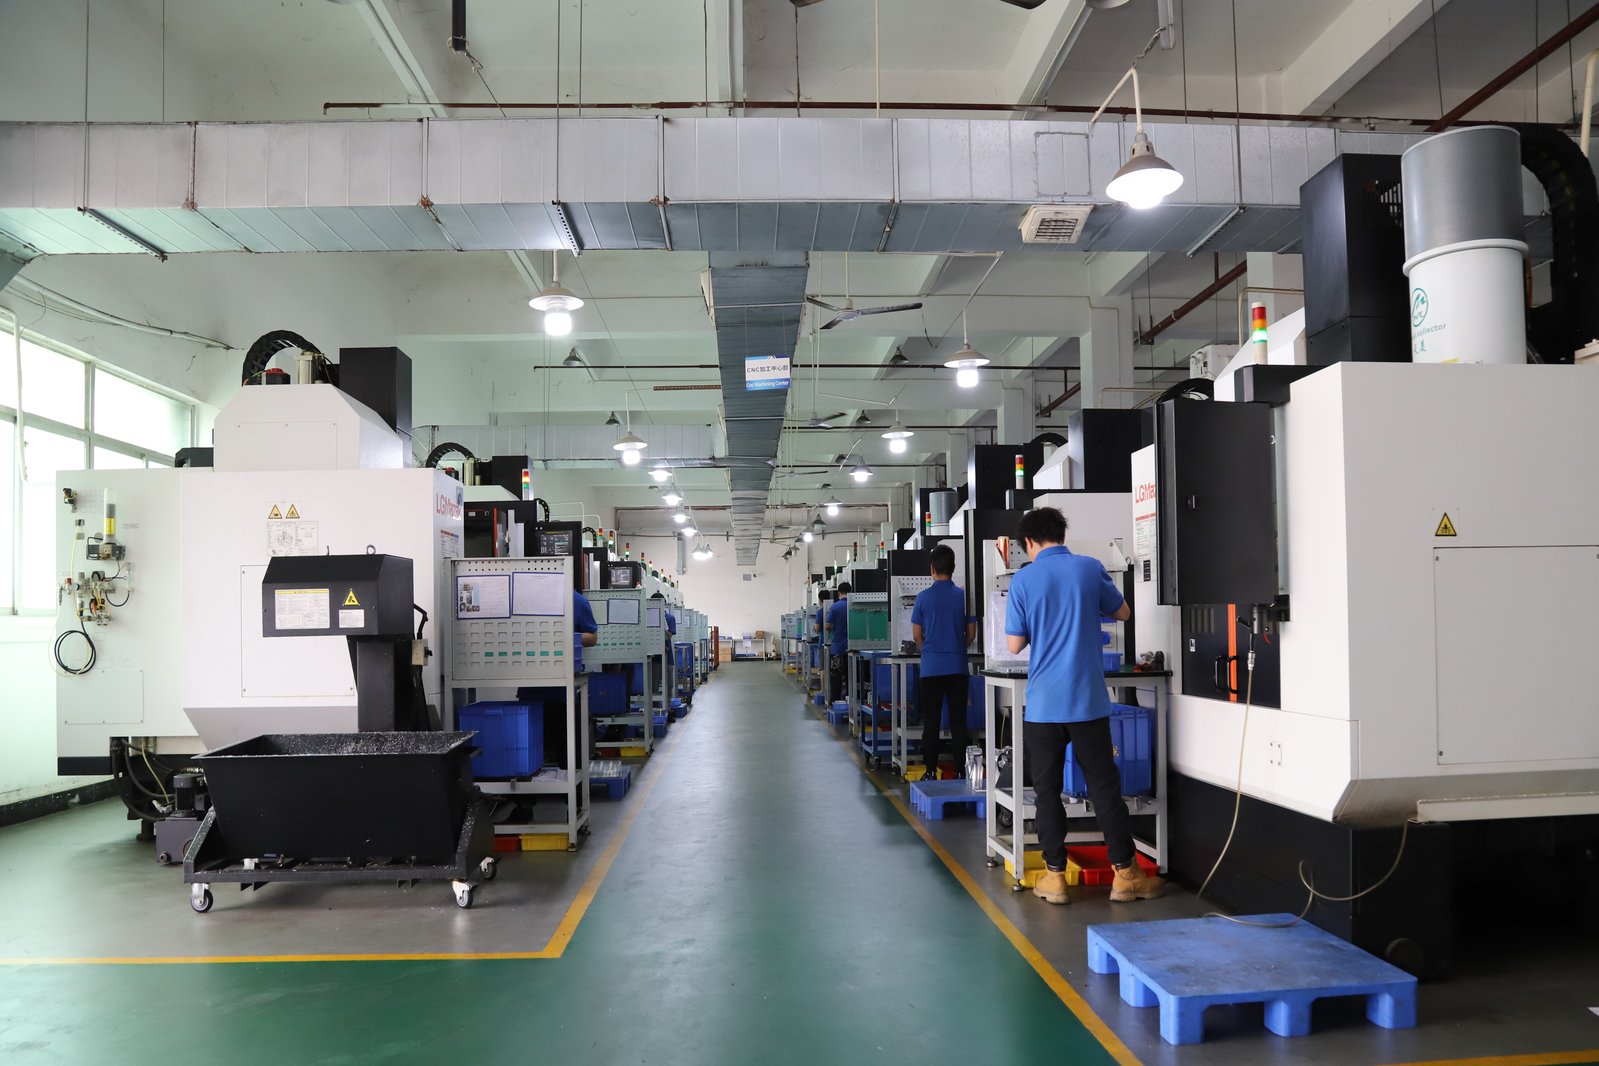
Aerospace components machined in China are build-to-print work: your organization holds the design, the analysis, and the qualification data, while the supplier buys the alloy, holds the geometry, and documents the result. The machining runs inside the same controlled envelope as good commercial work - ±0.003 mm on milled and turned features and ±0.002 mm on precision-ground surfaces - but the record carries more weight across an ocean: material traceable to a heat, inspection tied to the drawing revision, and change control that survives an audit. This guide lays out the materials, documentation, and tolerance decisions to make before you source aerospace CNC machining from China.
- Alloys to name: 7075-T6 and 2024-T351 aluminum, Ti-6Al-4V, 17-4 PH, and Inconel 718 where temperature demands it.
- Tolerance envelope: ±0.003 mm milled and turned features, ±0.002 mm precision-ground surfaces, capability Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window.
- Proof to require: a mill certificate with heat number, a CMM report against the drawing datums, an FAI for the first lot, and written deviation records.
- AS9100: the aerospace quality framework; verify documentation and change control in practice, then check the base certifications underneath.
What changes when a machined part enters an aerospace program?
Aerospace machining is build-to-print work. The prime or the equipment maker holds the design and the qualification data, while the CNC machining supplier in China buys the alloy, cuts the geometry, and documents the result. What changes for the supplier is the burden of proof attached to every lot, and distance makes that record the only evidence you have.
Three disciplines carry the burden. Incoming alloy must be verified before cutting, not trusted on paper. Inspection must be measured against the drawing revision and its datum reference frame, so position is checked as position and profile as profile. And change control must be explicit, because a silent substitution of barstock or coating can invalidate data already qualified for flight.
None of these habits require exotic machines. They require a shop that treats the drawing as a contract, quarantines incoming material until it is proven, and writes down every deviation. Those habits are visible in the first design review, which is why the review matters more than the price on a first aerospace order.
Distance makes the disciplines more visible, not less. Because you cannot walk the floor, every claim arrives as a document, and the quality of the paperwork becomes the quality signal. A supplier whose files are consistent, dated, and traceable is running a controlled process; one whose files are generic is not - and the first review exposes which kind you are dealing with.
Which alloys and product forms should an aerospace drawing name?
The material callout fixes the qualification you have already run, so it must name the exact grade, temper, product form, and certificate requirement. The table below covers the common machined aerospace alloys and what each one demands of the drawing.
Confirm that the drawing note and the quoted grade match, because a mismatch between the note and the certificate is the most common material failure in aerospace sourcing.
| Alloy | Where it is used | What to specify |
|---|---|---|
| 7075-T6 aluminum | Structural brackets, fittings, frames | High strength with good machinability; confirm grain direction where analysis requires it. |
| 2024-T351 aluminum | Tough, fatigue-resistant airframe parts | Lower corrosion resistance than 7075; pair the temper with the right finish. |
| Ti-6Al-4V (Grade 5) | Load-carrying brackets and fittings | Machines slowly; budget longer cycles and a clear premium over aluminum. |
| 17-4 PH stainless | Actuator and mechanism hardware | Name the condition so the certificate proves the hardened state. |
| Inconel 718 | High-temperature hardware | Severe work hardening; reserve for parts that genuinely see the temperature. |
State the product form - bar, plate, or forging - because grain structure and property basis are part of the design allowables. Write the full callout, for example 7075-T6 plate with a mill certificate required, so the quote prices the correct stock and the certificate states the form that was actually machined.
Ask the supplier to confirm it can source the named form with a certificate before you commit. Plate and bar are routine; a specific forging or an uncommon temper can add weeks to procurement. A shop that checks material availability at the quoting stage is managing your schedule rather than discovering it later.
One distinction worth making early is machined-from-stock versus forged. If the drawing assumes a forging for grain flow, the supplier must quote the forging blank plus the machining, and the certificate must trace the forging heat. Confirm the product-form assumption before the quote - a mismatch between the stock ordered and the form the analysis assumed is a design-data failure, not a shop issue.
How do you verify the material machined matches the drawing from a distance?
A certificate proves little until the shop connects it to the metal being cut. The control loop runs on the floor: incoming stock is quarantined, the heat number on the certificate is matched to the marks on the bar or plate, and an alloy check - typically XRF - is run before material is released to a machine.
Audit the loop by email and video. Is a certificate kept per heat number and linked to the parts from that lot? Is the incoming material physically checked against the certificate, or only matched on paper? Can the supplier produce the certificate for the exact lot that ships, rather than a generic type certificate?
Then require the certificate, with its heat number, to be attached to the first-article report. Years later, when an auditor asks where a component came from, that attachment is the answer - and in aerospace, a missing heat number is not a filing gap but the start of an investigation.
Clarify which certificate level you will accept before ordering. A certificate of conformance is a supplier declaration; a mill certificate in the EN 10204 3.1 style reports the actual test results for the heat. Naming the level in the RFQ prices the paperwork into the quote.
What tolerance can an aerospace drawing realistically demand?
The realistic envelope is the one serious shops use everywhere: ±0.003 mm on milled and turned features and ±0.002 mm on precision-ground surfaces that seat or seal. What changes in aerospace is the acceptance standard - capability at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window., demonstrated from the first article rather than assumed.
Geometry limits the envelope as much as the numbers. Thin webs, deep pockets, and long unsupported walls flex under cutting force, so a tolerance written on paper must survive the process that makes the part. A shop that reads drawings flags those features in the design-for-manufacturing review before quoting.
Tolerance only what the function needs, and measure what you tolerate. Because aerospace drawings are built on GD&T, acceptance belongs on a CMM against the datum reference frame, not on hand tools at the bench. Put the measurement method in the order so the acceptance test is fixed.
Measurement uncertainty deserves a line in the conversation. A CMM reading carries its own error, and when the tolerance band is thin the gap between the reported value and the true value starts to matter. A shop that can discuss that margin is measuring seriously, and its report should name the instrument.
What documentation should travel with an aerospace lot?
Agree the document package before you order, because records planned in advance are stronger than records reconstructed after shipment. For build-to-print aerospace work from China, a practical minimum:
- Material certificate for each heat number used, naming the alloy, condition, and product form on the drawing.
- Certificate of conformance confirming the parts were machined, inspected, and finished to the released revision.
- CMM and instrument reports measured against the drawing datum reference frame, with roughness data where Ra is specified.
- First-article report for a new part, plus SPC data on key characteristics where the program requires it.
- Deviation or non-conformance record for anything that left nominal, agreed before shipment.
Keep the approved FAI and certificate from the first lot as the reference sample, and require the same configuration on repeat lots. The quality page on this site lists the CMM, surface, and vision instruments behind those reports and how data is linked to each lot.
For multi-lot programs, ask for certificates consolidated by heat number across deliveries. Comparing the same heat across purchase orders can expose a material problem early, before it spreads through three shipments and into your build schedule.
Ask which documents the supplier can regenerate years later and how long the records are retained. In aerospace the traceability must outlive the program, and a retention policy written into the supplier agreement protects you long after the last lot ships, when the audit may come looking for them.
What does AS9100 ask of a China machining supplier - and what should you audit?
AS9100 is the quality standard that aerospace primes and their supply chains expect component makers to operate under or align with. For a build-to-print machine shop the relevant parts are document control, controlled purchasing, lot traceability, change and deviation notification, and calibration records.
The shop does not hold your design or qualification data; you do. When you evaluate a China CNC machining supplier for aerospace work, ask how its processes line up with AS9100 expectations and verify the quality system underneath - ISO 9001:2015, IATF 16949:2016 (product design excluded) and ISO 14001:2015 certified is the base you should see in writing.
Then audit behavior rather than badges. Ask for a sample first-article report, a written change-notification procedure, and a copy of the last non-conformance record. Those documents show how the shop behaves when something goes wrong - which is exactly when aerospace suppliers earn their place on your list.
Keep the audit evidence in one file per supplier. When the next program arrives, the review becomes a checklist refresh rather than a re-investigation, and the accumulated documents give you a trend line that a single audit never provides.
What finish and edge callouts matter on a machined flight part?
Finish on a flight part is a functional attribute. Machined surfaces sit in fatigue paths, seal against fluid, or carry fasteners, and a burr or torn edge is a defect that can fail in service. Practical values run in the familiar precision bands: milled and turned faces between Ra 0.8 and Ra 3.2 µm, with ground details reaching lower where they seat or seal.
Secondary processes complicate the callout. Anodizing, passivation, plating, and shot peening change the surface after the tool leaves it, so a drawing that demands Ra 0.8 µm after anodizing is a different job from one that expects it straight from the machine. State whether the value applies before or after finishing.
Fatigue is where the discipline pays. A rough scalloped floor or a torn edge in a load path concentrates stress far beyond the drawing nominal. If the analysis assumes a machined finish, the shop should verify the cutter path leaves a surface consistent with that assumption.
Decide how finish and corrosion protection interact before ordering. Aerospace parts rarely fly bare: anodizing, passivation, plating, or primer follow machining, and each can shift dimensions and alter the surface. Confirm where the measurement happens in the sequence and which configuration the tolerances apply to.
How do you qualify a China machining supplier for aerospace work remotely?
- Send a real drawing and ask for a technical review. The response should name thin walls, datums, and material condition - the features that decide machinability.
- Request the documentation package before you commit. Ask for a sample FAI and the material certificate format.
- Probe material control. Ask how incoming alloy is verified, how heat numbers link to lots, and how long records are kept.
- Verify the quality system and its audit trail. Read the certificate scope, then ask to see inspection reports from a recent aerospace-style lot.
- Run a small first lot before you scale. Inspect the records as hard as the parts; the paper trail is the deliverable that scales.
Qualification is a loop rather than a single audit. First lot, review the FAI and the certificates, then release a larger batch and compare the documentation on both. Within two cycles you will know whether the supplier treats aerospace paperwork as overhead or as the product.
Include the sample parts in the plan: first-article components count toward your total and ship with the lot once approved. Agree who owns the samples at the quoting stage, so there is no surprise on the invoice.
Frequently Asked Questions
Do aerospace parts need tolerances tighter than ±0.003 mm?
Milled and turned features hold ±0.003 mm in a controlled process, and precision-ground surfaces reach ±0.002 mm. Capability at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window matters more than a headline number.
Which material certificate should an aerospace order carry?
A mill certificate in the EN 10204 3.1 style naming the producer, the heat number, and the test results for that heat. The heat number must match the stock used for your lot and should attach to the first-article report.
Can a China CNC machining supplier make aerospace components?
Yes, as a build-to-print supplier. Shops with controlled processes, verified material, and disciplined documentation routinely produce aerospace brackets and housings while the customer keeps design and qualification responsibility.
What is the difference between 7075 and 2024 for a machined part?
7075 gives higher strength and suits structural brackets; 2024 gives better toughness and fatigue resistance but lower corrosion resistance. Name the temper and the protective finish.
Why do thin walls cause problems in aerospace machining?
Thin walls and deep pockets flex under cutting force, so the tolerance on paper cannot be held unless the shop controls tooling, stepover, and fixturing. A good review flags these features before quoting.
Is AS9100 certification required from a machining supplier?
Primes commonly expect suppliers to operate under or align with AS9100, but the requirement lives in your contract and supplier agreement. Verify documentation and change control in practice.
What should an aerospace first-article report include?
A measurement of every feature against the drawing datum reference frame, the drawing revision and material heat number, and the certificate for the lot. If the FAI cannot be mapped feature by feature, the process has not been demonstrated.
Have an aerospace drawing that needs a documentation review?
Send the part file with your material and certificate requirements and ask for a technical review before you commit. Contact the CNC Machining China team to start the conversation.