
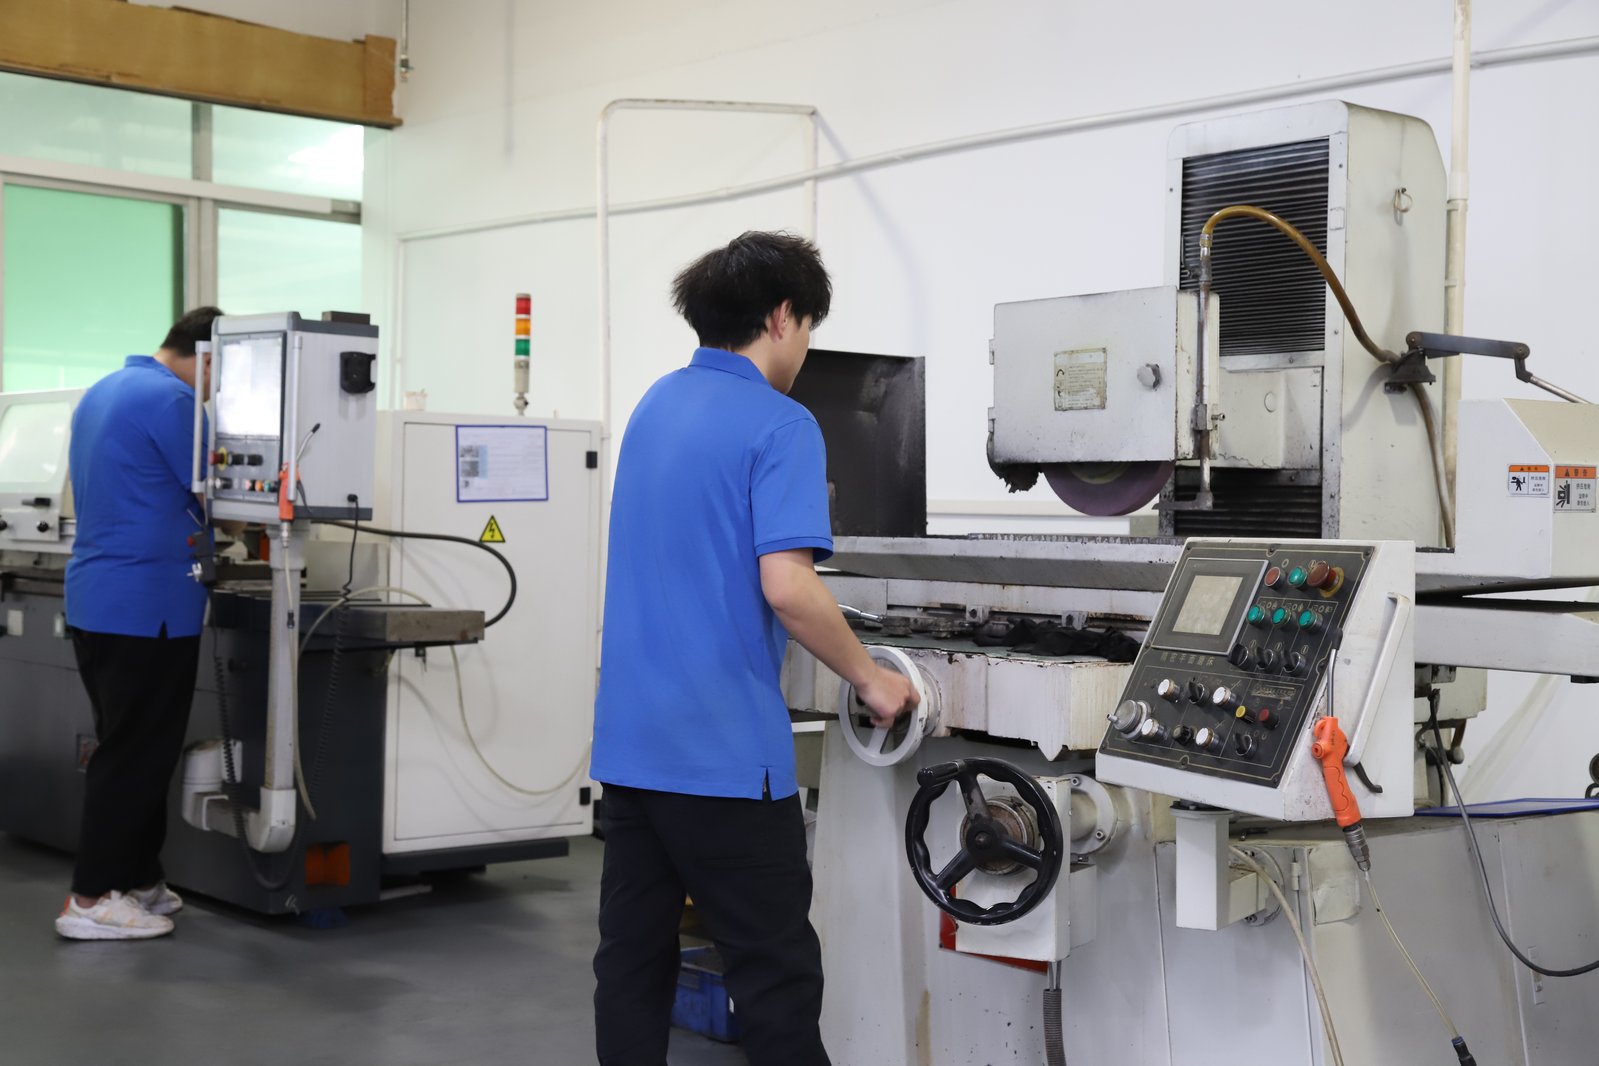
Every machined part carries two kinds of callouts: size and form tolerances that define the geometry, and surface finish values that define the texture. Both are achievable inside a known envelope - ±0.003 mm on milled and turned features and ±0.002 mm on precision-ground surfaces, with finishes from a fine machined surface to a mirror polish - but each one adds cost in cutting strategy and inspection. This guide explains what a China CNC machining supplier can realistically hold, how to specify it so the drawing is clear, and where the money goes.
- Tolerance envelope: ±0.003 mm on milled and turned features, ±0.002 mm on precision-ground surfaces, Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window.
- Surface range: machined surfaces commonly run Ra 0.8-3.2 µm, with ground details reaching lower.
- Specify by function: tighten and smooth only the features that mate, seal, or carry load.
- Measure as specified: the drawing should state whether roughness applies as machined or after finishing.
- Verify on the report: tolerances and Ra belong on the inspection report with the instrument named.
What tolerance can a China CNC machining shop realistically hold?
The honest production envelope is ±0.003 mm on milled and turned features in a controlled process, with precision-ground surfaces reaching ±0.002 mm where they seat or seal. Claims tighter than that are either grinding with extra steps or marketing, and drawings should not be built around them unless the process genuinely earns it.
The acceptance criterion matters more than the headline number. Capability at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window means the process holds the band lot after lot, not that a sample happened to land inside it. Ask for capability data on the critical features, not for a promise.
Ask for the capability report as part of the quotation on the first order. A shop that can show Ppk ≥ 1.67 initial from a previous run of a similar part is measuring its process; one that cannot will ask you to trust it until the first article arrives.
Tolerance on a machined part is not one number; it is a profile across the drawing. A bore that mates a bearing holds ±0.003 mm; a cosmetic face can run ten times looser. Specifying each feature at the tolerance its function earns is how you control both cost and risk.
Agree the general tolerance block with the shop before quoting. A drawing that leaves the block blank lets every supplier interpret the rest of the part differently, and the interpretation shows up on the invoice rather than on the drawing.
Why do tight tolerances cost more on a machined part?
Every tight callout changes the cutting strategy: slower finishing passes, dedicated tooling, and measurement against the datum structure. On a mill, position and form add workholding and tool-path planning; on a lathe, roundness and concentricity add their own requirements. Each adds cycle time.
Thin walls and deep pockets are the hard cases for both tolerance and finish. Sections flex under the tool, so tight callouts on unsupported features need careful stepover and fixturing - and the quote should reflect that care rather than discover it on the first article.
Inspection adds a second layer of cost. A ±0.003 mm feature is verified on the instrument the drawing implies, and GD&T callouts like position and profile need CMM verification against the datum reference frame. Every tight characteristic is a line in the report.
Measurement uncertainty belongs in the plan. A CMM reading carries its own error, and near the edge of a ±0.003 mm band the difference between the reported value and the true value matters. Ask how the shop handles that margin before the first article is measured.
The drawing discipline that saves money is the same everywhere: hold the tight band on the features that mate, seal, or carry load, and release everything else to a sensible general tolerance. Mark the key characteristics so the shop concentrates its measurement budget where the part needs it.
Which surface finishes are achievable on a machined part?
Machining produces a range of finishes depending on the process, material, and cutting parameters. Milled and turned surfaces commonly land between Ra 0.8 and Ra 3.2 µm, with finishing passes reaching the finer end. For smoother surfaces, grinding moves toward Ra 0.2-0.8 µm and polishing beyond.
Ask what finish the standard quote assumes. Many shops include a fine machined surface by default and price better finishes as options, so knowing the default stops the surprise when a tighter Ra appears on the invoice.
| Surface | Typical Ra range | Where it is used |
|---|---|---|
| Rough machined | Ra 3.2 µm and above | Non-critical faces, stock removal before finishing |
| Fine machined | Ra 0.8-1.6 µm | Sealing and sliding faces, general precision work |
| Ground | Ra 0.2-0.8 µm | Bearing seats, seal surfaces that must be precise |
| Polished / lapped | Below Ra 0.2 µm | Optical and high-wear surfaces, appearance parts |
Process and material move the achievable finish. A milled face reaches a different texture than a turned one, and aluminum finishes more easily than stainless. If the drawing calls a tight Ra on a difficult material, expect slower finishing passes.
Finish and tolerance interact on the same feature. A surface that must seal needs both the tight dimension and the fine Ra, and the two callouts are verified separately - size on the gauge, roughness on the tester. Make sure both appear in the inspection report.
How should you specify surface finish on a drawing?
Name the value, the direction, and the timing. The value is the Ra target, direction tells the shop whether lay matters, and timing decides whether the Ra applies as machined or after anodizing, plating, or passivation - because each coating changes the surface after the tool leaves it.
A finish callout without a timing note is a dispute waiting to happen. A drawing that demands Ra 0.8 µm after anodizing is a different job from one that expects it straight from the machine, and the coating thickness alone can change the measured surface. State which applies.
Where a finish follows a coating, ask who measures and when. The shop may verify roughness as machined and rely on the coating house for the final surface, and the acceptance should name the step that owns the number.
Function should set the finish, not habit. Sliding and sealing faces earn a real Ra with inspection to back it; faces that simply close a profile do not. Specify finish by function and the price follows the drawing.
Lay direction matters on some sealing and sliding surfaces. If the function is sensitive to the direction of the machining marks, note it on the drawing; a ground or polished detail may need an extra operation to reach the lay the design assumes.
How are tolerance and finish measured on machined parts?
Size is measured on the instruments the tolerance implies, and GD&T callouts are verified on a CMM against the datum reference frame. Roughness is measured with a surface tester that reports Ra over the evaluated length. Each method has its own report line.
The report should state the instrument, the operator, and the calibration date for every critical characteristic. A dimensional report without provenance is a form to be filled, and the first-article report should map feature by feature to the drawing so you can verify the claims.
Include the surface-lay callouts in the measurement plan. Where lay matters, the report should confirm the direction of the marks as well as the Ra value, because the texture direction is part of the function.
Capability data is the bridge between a sample and a process. If the drawing demands Ppk ≥ 1.67 initial on a key feature, the shop should report the SPC data across the lot, not just the first article. That is the difference between measuring parts and measuring the process.
Calibration records for the measuring equipment are reasonable to request before a tolerance-critical order. A CMM out of calibration makes every report fiction, and the calibration date is the one line that tells you the numbers can be trusted.
Where do form and position fit into the tolerance story?
Machined parts are defined by more than size. Flatness, parallelism, position, and profile describe the form of the part relative to its datums, and they are often the callouts that decide whether an assembly fits. These are measured against the datum reference frame, not against a caliper reading.
Position readings are only as good as the datums they reference. The drawing should define datums that are machinable and measurable, and the report should state the datum order used on the CMM, because a different datum order changes the numbers.
Holding form comes from the process: workholding, tool-path strategy, and thermal control all affect it. Thin walls and deep pockets flex under cutting force, and interrupted cuts from holes and slots distort sections. A shop that flags those risks in the design review is protecting the drawing.
Specify form callouts where the function demands them and leave the rest to the general tolerance block. A drawing covered in position callouts on every feature pays for measurement the function never uses.
Ask how the shop measures form - on a CMM for position and profile, on the appropriate gauge for size. The instrument decides what the number means, and a supplier that names its method is planning the measurement rather than hoping.
How does material affect achievable tolerance and finish?
Aluminum conducts heat away and cuts cleanly, which makes fine finishes and stable thin sections easier to hold. Stainless work-hardens, so tight tolerances and fine finishes need more careful feeds. Titanium and the nickel alloys are harder still, and each step up in difficulty adds cycle time.
The tolerance envelope does not change with material - ±0.003 mm is achievable across the common machined alloys - but the cost to reach it does. The same drawing in 316L costs more to hold than in 6061, and the drawing review should say so.
Thermal effects matter on precision work. Aluminum expands roughly twice as much as steel per degree, so tight features measured in a warm shop can drift with the temperature. Shops that hold ±0.003 mm control the environment around the measurement as well as the cut.
When a drawing mixes materials, note that each holds the same envelope but at a different cost and cycle. Let the quote show the per-material difference so the choice is visible before the order rather than after it.
How do you turn tolerance and finish into a quotation?
- Mark the key characteristics. Flag the few features that must hold ±0.003 mm or a tight Ra, and leave the rest to general tolerances.
- State finish timing. Say whether Ra applies as machined or after anodizing, plating, or passivation.
- Name the measurement method. Agree which instruments verify the critical callouts so the acceptance test is fixed.
- Ask for capability data. Request Ppk ≥ 1.67 at the initial study on the key characteristics from the first article forward.
- Request the itemized split. Tolerance and finish cost should be visible in the quotation, not hidden in the total.
Tolerance and finish are not mysteries to be discovered after the order; they are callouts to be agreed before it. When the envelope, the method, and the cost are on the table, the drawing becomes a contract both sides can measure against - and the first lot proves it.
How do you lock tolerance and finish into the first-article approval?
The first article is where tolerance and finish claims meet reality. The FAI should verify every critical callout - size on the gauge, form and position on the CMM, roughness on the surface tester - and map each reading to the feature on the drawing. If the report cannot be mapped, the claim has not been proven.
Ask for the capability picture, not just the sample. The first article shows one part; the SPC data across the first lot shows whether the process holds the band. Demand Ppk ≥ 1.67 at the initial study on the key characteristics from the first lot forward, so the approval covers the run rather than the single piece.
Approve the sample in writing before production releases, and keep it as the reference for every later lot. When a subsequent delivery arrives with a different finish or a drifted dimension, the approved sample and its report are the comparison that settles the argument.
Reconfirm the envelope on every reorder. Tooling wears, materials change suppliers, and the capability that held last year needs re-proving; a fresh SPC run on the first lot of every new program is the cheapest insurance you can buy.
Frequently Asked Questions
What tolerance can a China CNC machining shop realistically hold?
Milled and turned features hold ±0.003 mm in a controlled process, and precision-ground surfaces reach ±0.002 mm. Capability at Ppk ≥ 1.67 at the initial study on key characteristics and Cpk ≥ 1.33 on general characteristics. Capability is reported per characteristic: every report names the feature, its tolerance band, the sample size, the sigma method, and the study window keeps the process passing lot after lot.
What surface finish can a machined part achieve?
Machined surfaces commonly run between Ra 0.8 and Ra 3.2 µm, with grinding reaching Ra 0.2-0.8 µm and polishing lower. Aluminum finishes more easily than stainless at the same Ra.
Does a tighter tolerance always cost more?
Yes, in cutting strategy and inspection. Every tight callout slows the finishing passes and adds measurement. Tighten the features that function and release the rest, and the cost follows the drawing.
Does surface finish cost extra?
A fine finish needs slower passes and often a finishing operation, and a ground or polished surface adds a process step. Finishes on functional faces are priced into the quote; ask what Ra is included.
How is roughness measured?
With a surface tester that reports Ra over an evaluated length. The report should state the instrument and where on the part the reading was taken, so the acceptance is verifiable.
What do flatness and position mean on a machined part?
They describe the form and location of features relative to the datum reference frame. Flatness measures the deviation of a surface, and position locates a feature relative to datums. Both are verified on a CMM.
Should finish be specified before or after coating?
The drawing should say which. Anodizing, plating, and passivation change the surface after the tool leaves it, so Ra as machined and Ra after finishing are different targets.
Want to know what your drawing can hold?
Send the drawing with your tolerance and finish callouts and ask for a design-for-manufacturing review that confirms the envelope and prices it. Contact the CNC Machining China team to start.